Why ASI parts last

Results first: what we measure on every chisel, then how we make it.

  • In-house heat treatmentCarburising, induction hardening, tempering and segment tempering
  • Zone hardness 55 / 50 / 45 HRCTip, middle, head on ASI 42CrMo4
  • Serial and heat numberMarked on every chisel
  • Making parts in AmbalaSince 2012

Hardness by zone

Drawing of a breaker chisel, head to tip, in three hardness zones
  1. Headabout 45 HRCTakes the piston blow without cracking
  2. Middleabout 50 HRCTough body that resists bending
  3. Tipabout 55 HRCHard working end that resists wear
ASI 42CrMo4, zone tempered. Target hardness by zone. Drawing, not to scale.

Every chisel is traceable

  • Dot-pin serial and model number
  • Heat number of the steel
[placeholder: hardness report per chisel: not issued today. Add a sample here if ASI starts issuing one]

How an ASI chisel is made

Six steps from bar to dispatch. We show what is done and measured, not settings.

  1. Bar cutting

    Bar stock cut to length on automatic and semi-automatic bandsaws.
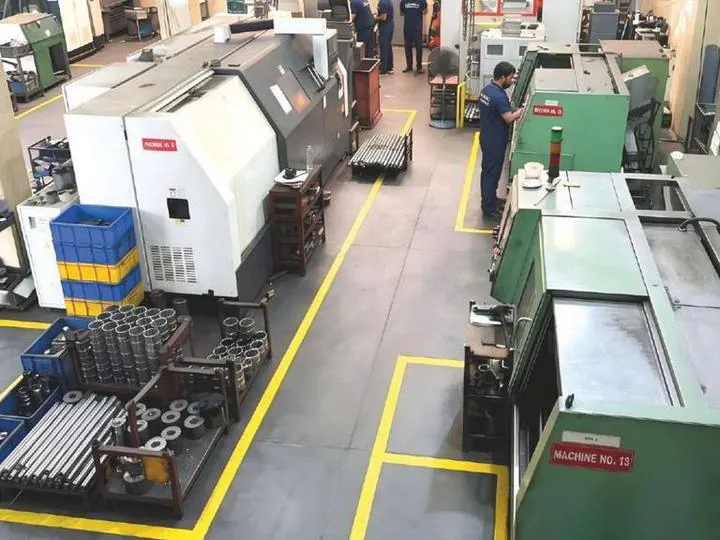
  2. CNC turning machines on the ASI shop floor

    Machining

    Turning on CNC turning centres; drilling, milling and grinding.
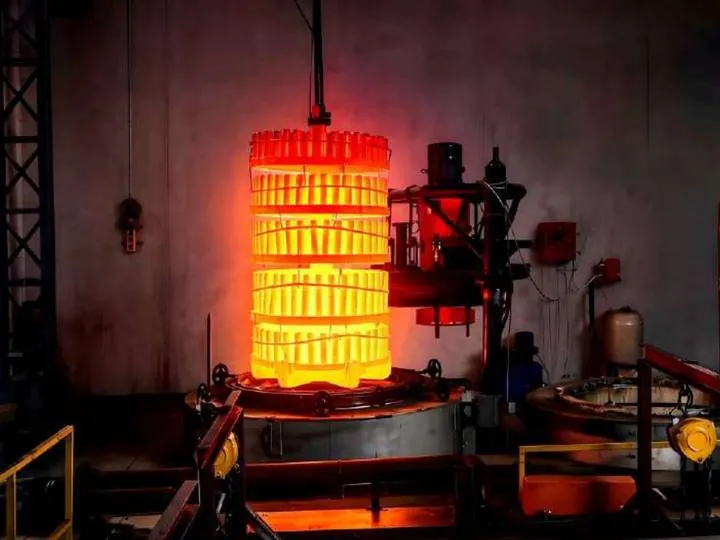
  3. Heat-treatment furnace in the ASI plant

    Heat treatment

    Hardening, carburising and induction hardening in our own plant.
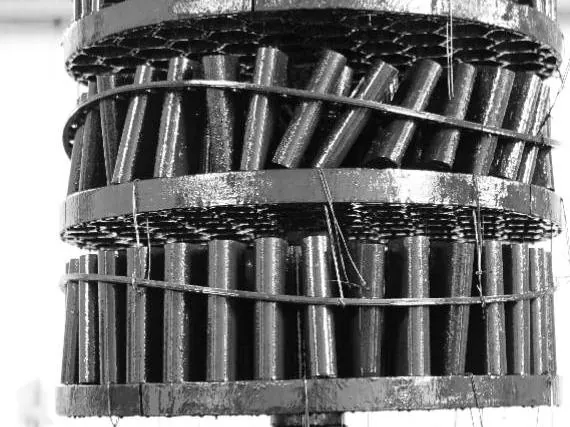
  4. ASI chisels loaded in a fixture for tempering

    Tempering and segment tempering

    Zone tempering gives each part of the chisel its own hardness.

  5. Testing

    Rockwell and portable hardness testing; hardness recorded by segment.
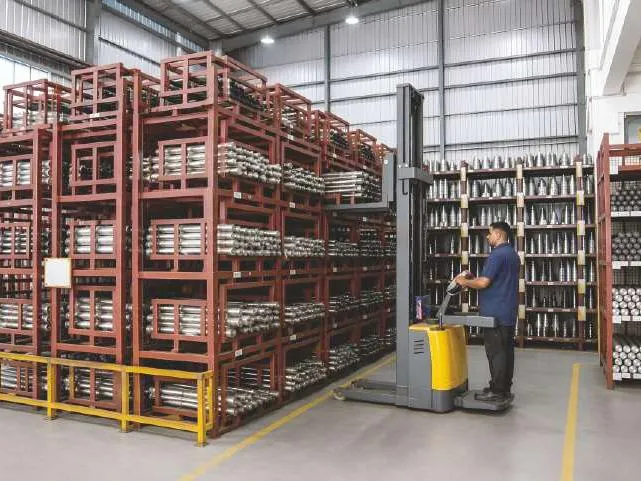
  6. Finished parts on storage racks in the ASI plant, Ambala

    Marking and dispatch

    Serial, model and heat number marked on every chisel before packing.

Hours before and after ASI

Customer-reported results on ASI parts. Customer names appear only with their permission.

  • Through bolts

    Before ASI
    300–400 h
    With ASI
    2,000+ h

    Working hours, as reported by a customer

  • Breaker bushes

    Before ASI
    500 h
    With ASI
    1,800+ h

    Working hours, as reported by a customer

  • Excavator pins

    Before ASI
    5–6 months
    With ASI
    18–22 months

    Service life, as reported by a customer

Plant and equipment

[placeholder: equipment table, re-checked by Vikrant: CNC turning centres and VMC count, grinders, gas carburising furnace (count to confirm), induction hardening, tempering, shot blasting, hardness testers, straightening press, bandsaws]
[placeholder: 60–90 s plant video, click to play with a poster image, never autoplay]

Certificates

MSME ZED certification, Silver

Ministry of MSME, Government of India

Number
[placeholder: certificate number]
Valid until
[placeholder: validity date]

PDF available on request

Exhibitions

[placeholder: exhibitions ASI has attended, with dates, re-checked from the current site]

Book a factory visit or ask for a price

We reply within 24 working hours, faster on WhatsApp.

WhatsAppCall
WhatsApp us